


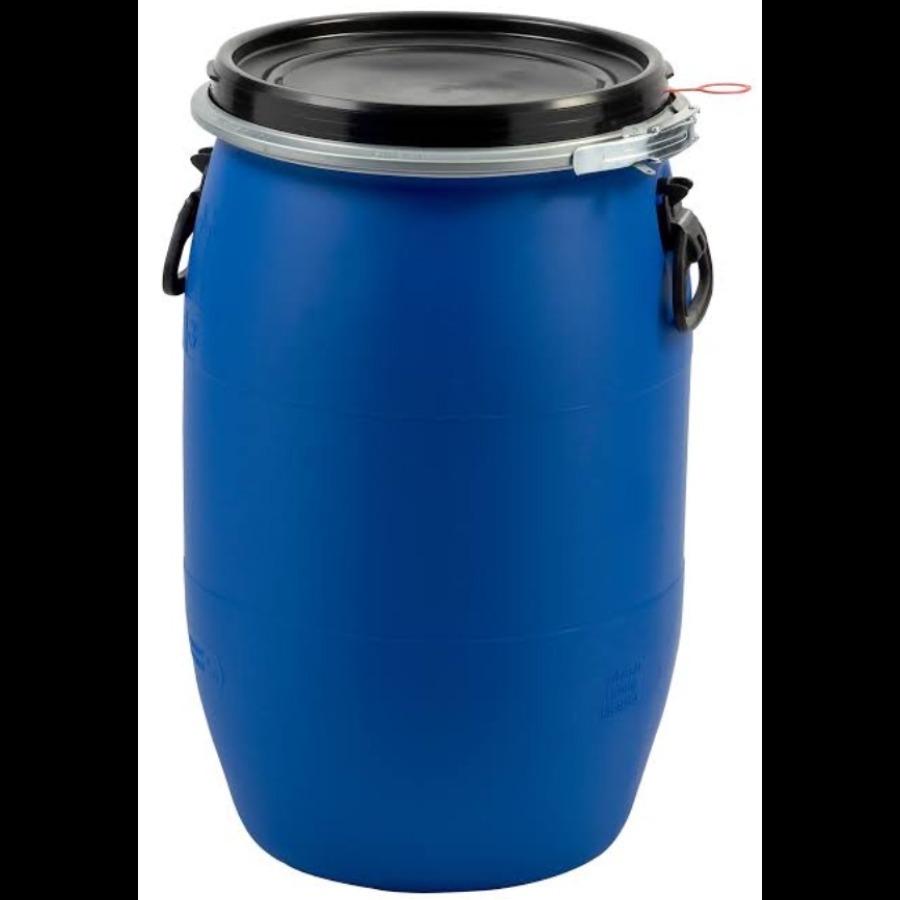
Transporting bulk liquids, acids, and industrial solvents demands containers that resist chemical degradation and physical impact. High-Density Polyethylene (HDPE) drums are engineered specifically to handle aggressive liquids without degrading or leaching.
Essential Features of HDPE Drums
Chemical Inertness: Polyethylene does not react with acids, alkalis, or organic solvents, preserving pure product chemistry during storage.
Seamless Blow-Molded Design: Monolithic construction eliminates side seams or joint welds, eliminating potential leakage points under hydraulic pressure.
UN-Certified Safety: High-grade HDPE drums undergo rigorous drop tests, stacking tests, and leak-proof tests to achieve UN ratings for dangerous goods transportation.
All-Weather Resilience: Unlike paper or metal containers, HDPE withstands rain, UV exposure, and high humidity without rusting or weakening.
The Takeaway
For chemical manufacturers and lubricant processors, HDPE drums remain the standard solution for risk-free bulk material transport.
